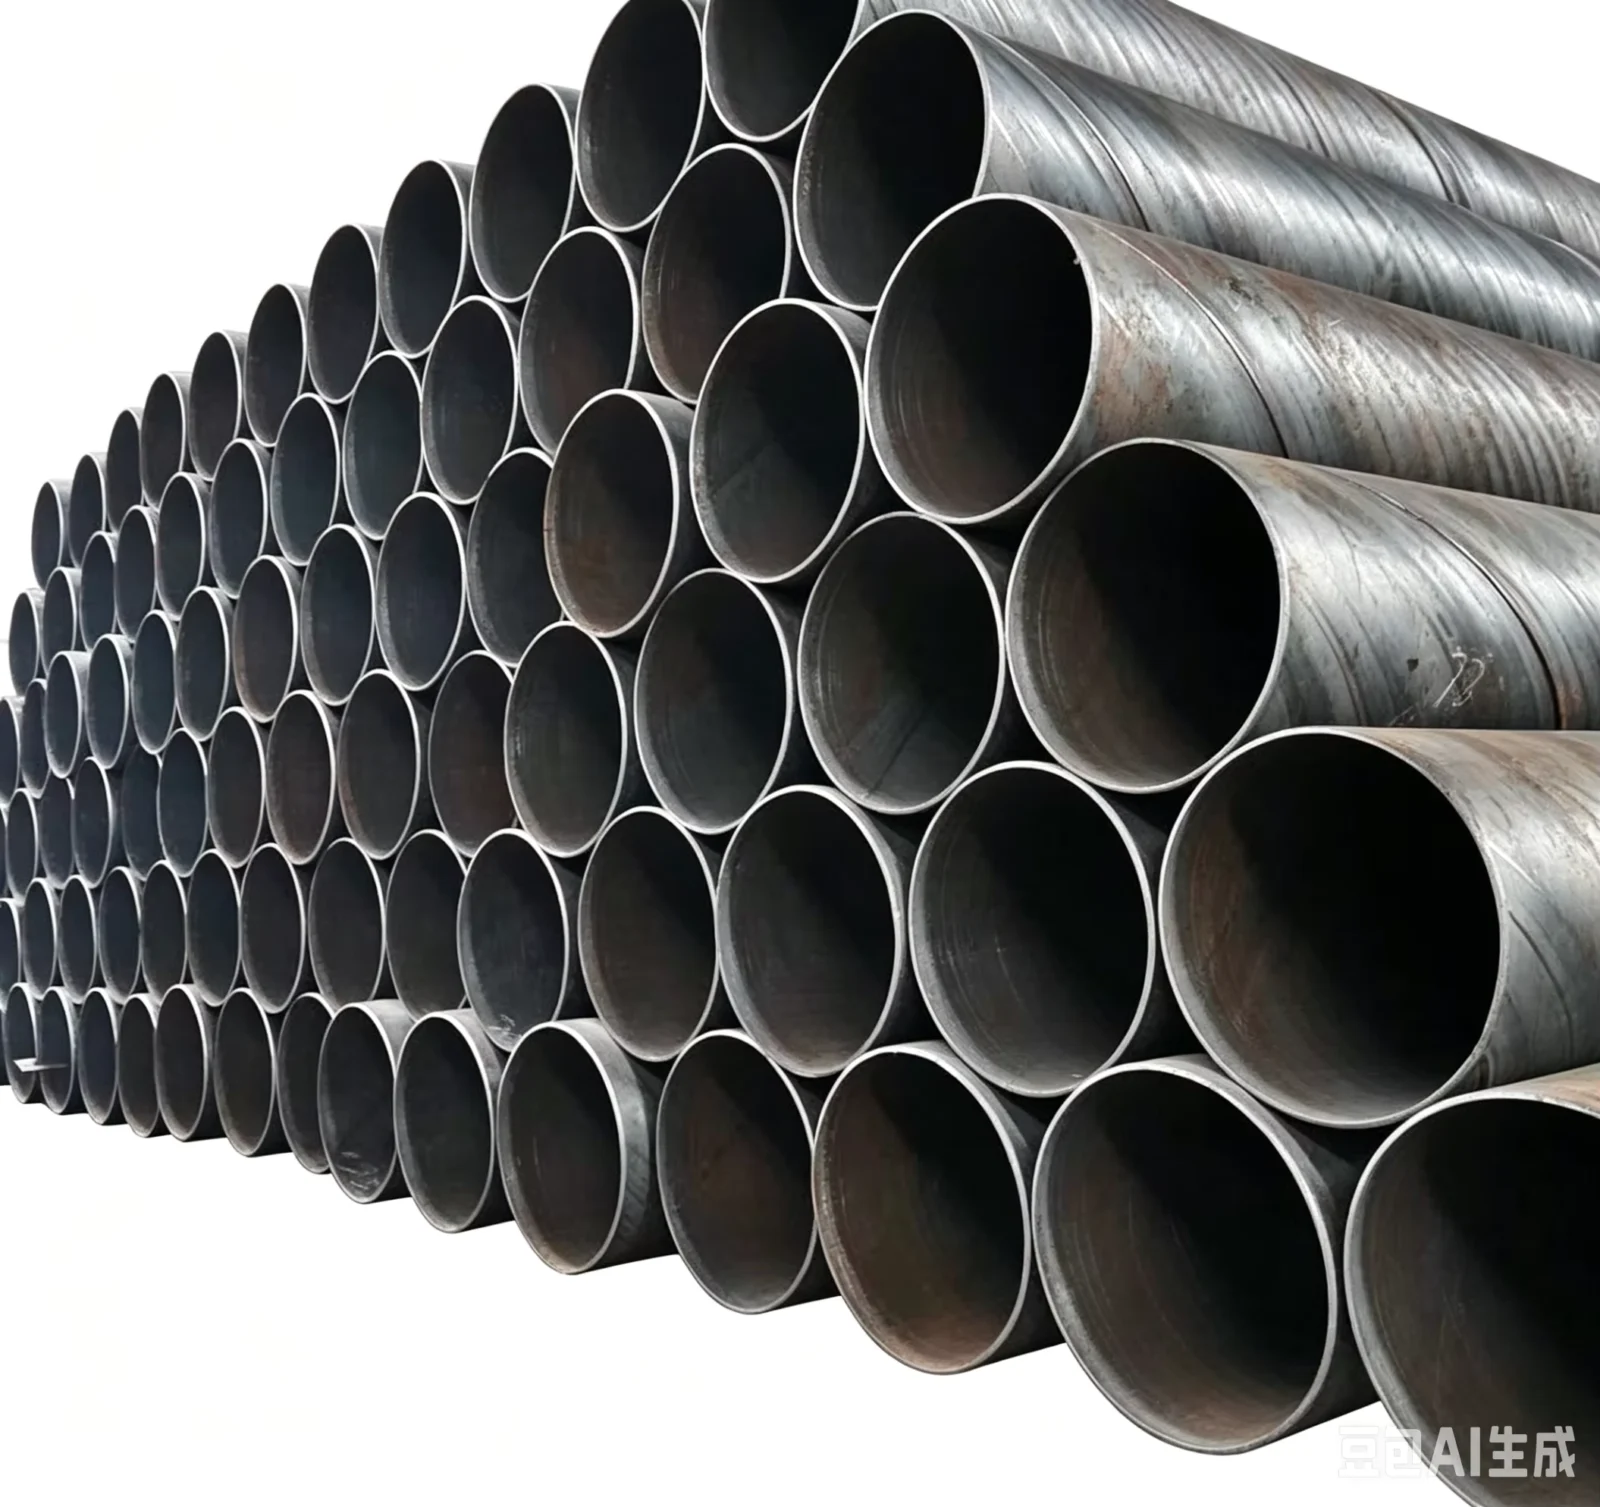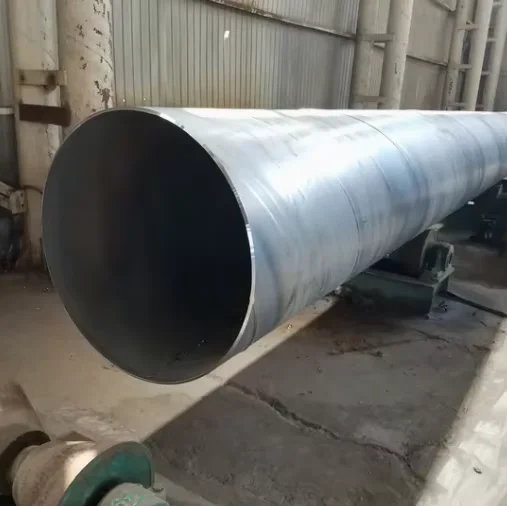
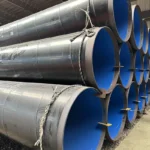
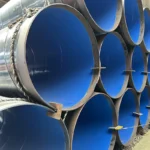
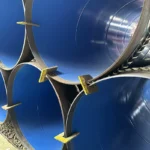
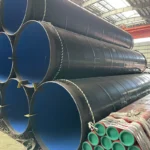
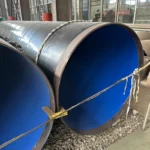
Description
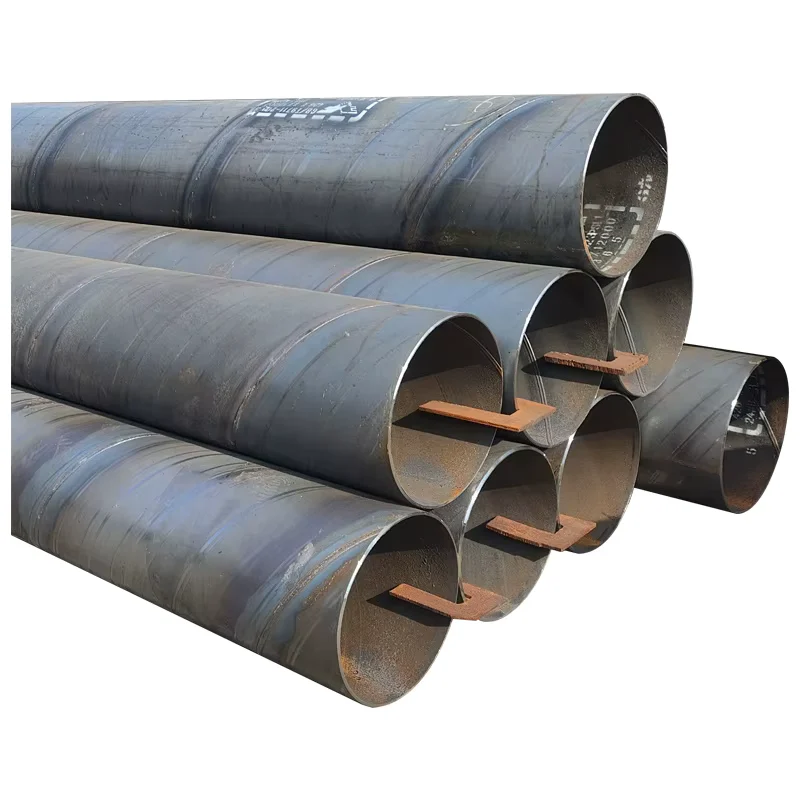
Direct Mill Supply for Large-Diameter Pipeline Projects — We manufacture Q235B and Q345B SSAW spiral welded steel pipe up to 2200 mm OD in-house, eliminating trader markups on heavy-wall pipeline orders.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | Q235B / Q345B SSAW Spiral Welded Steel Pipe |
| Product Type | SSAW Spiral Welded Round Steel Pipe |
| Steel Grade | Q195, Q235, Q345B, ASTM A53, A106, API 5L (X42–X80 / L175–L555) |
| Standard | API 5L, API 5CT, SY/T5037, SY/T5040, GB/T9711, ASTM A53, ASTM A106 |
| Section Shape | Round |
| Size Range | Outer Diameter 219.1–2200 mm |
| Wall Thickness | 3–30 mm |
| Length | 5.8–11.8 m (or as required) |
| Technique | SAW (Submerged Arc Welded) / Spiral Welded |
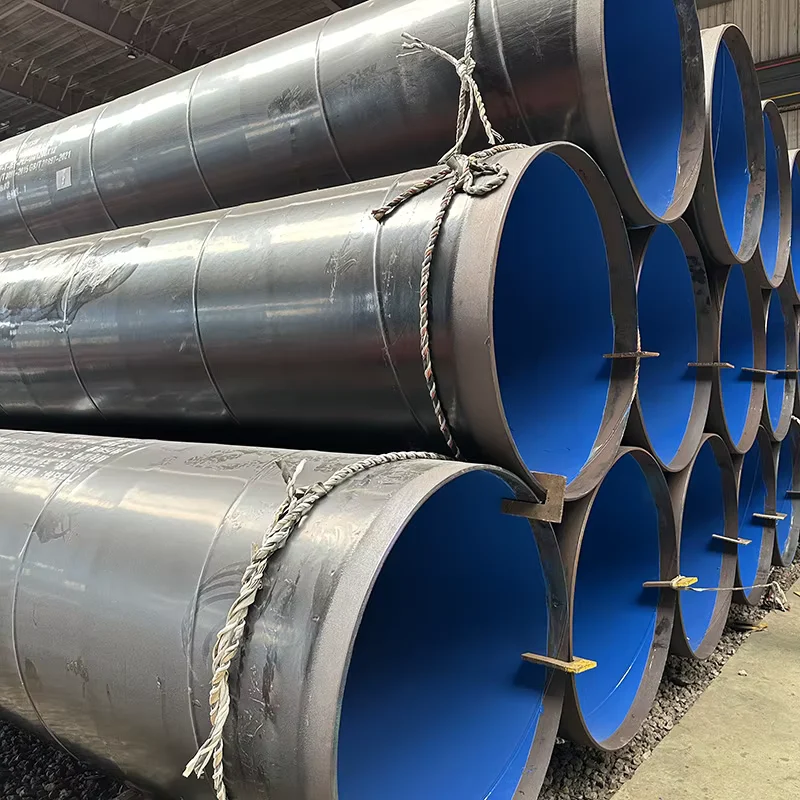
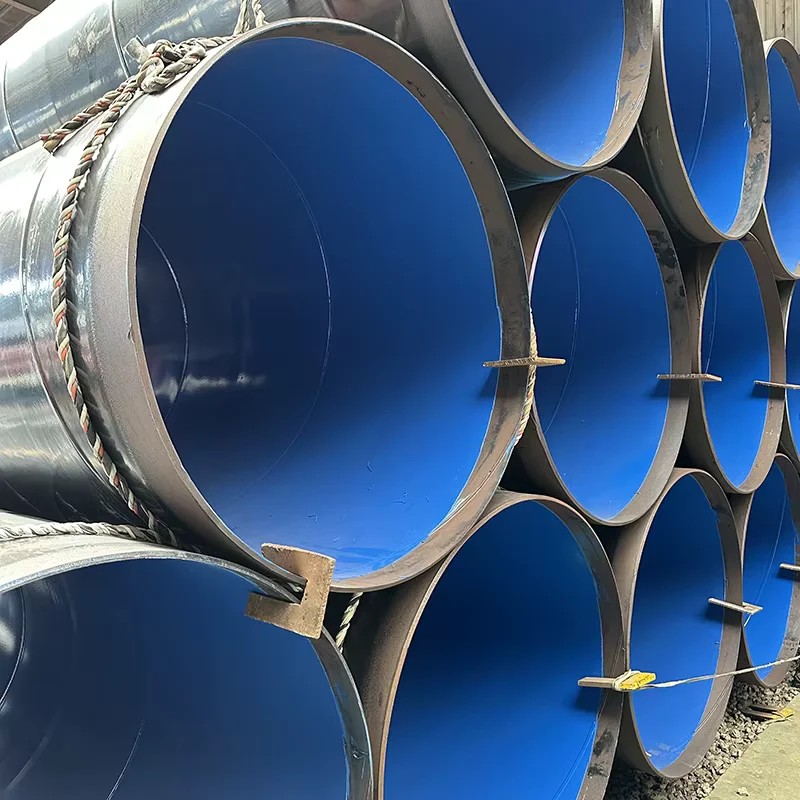
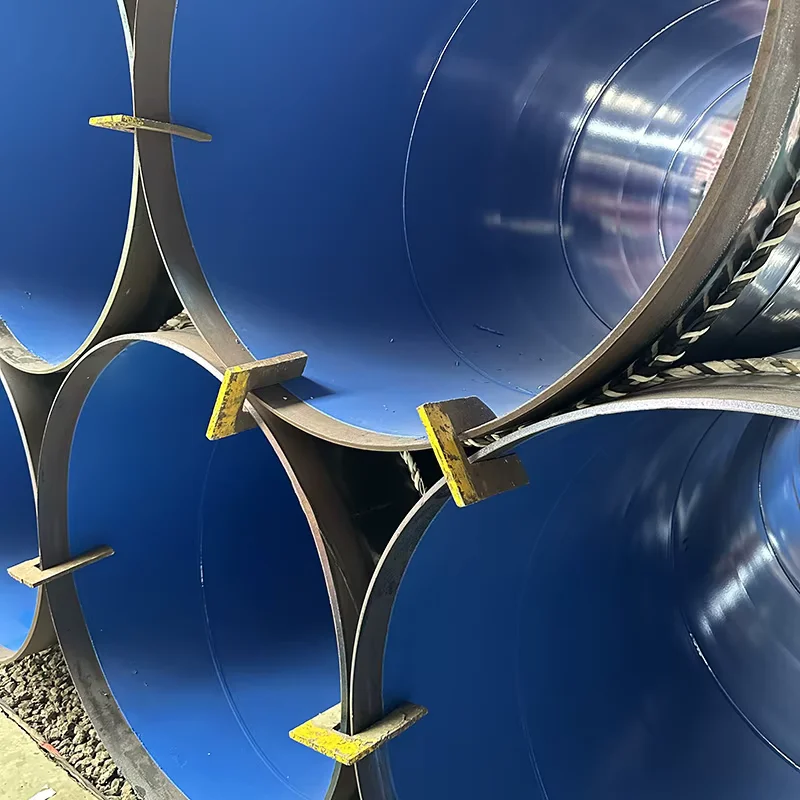
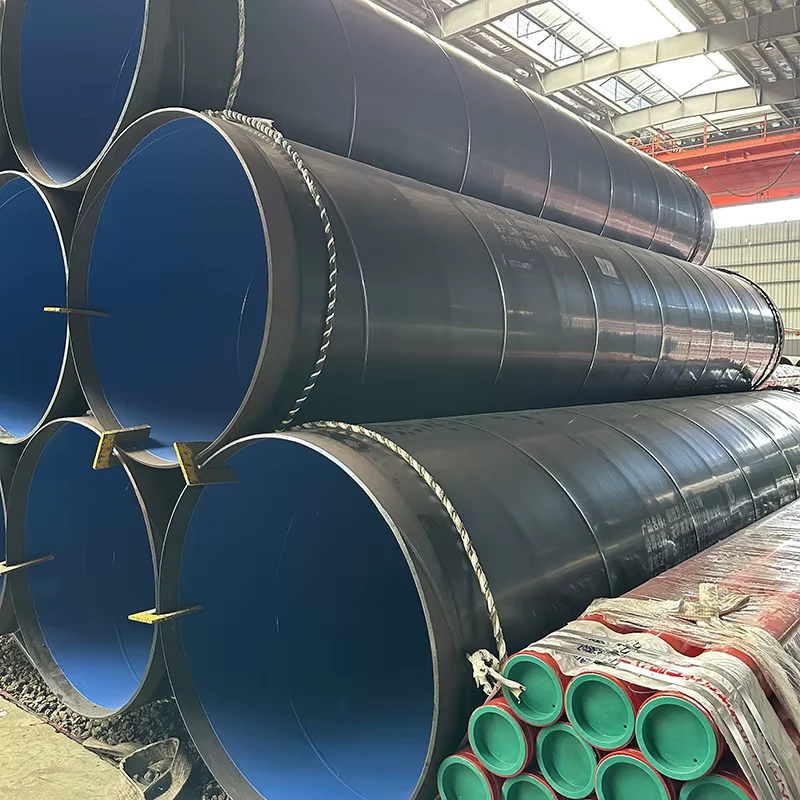
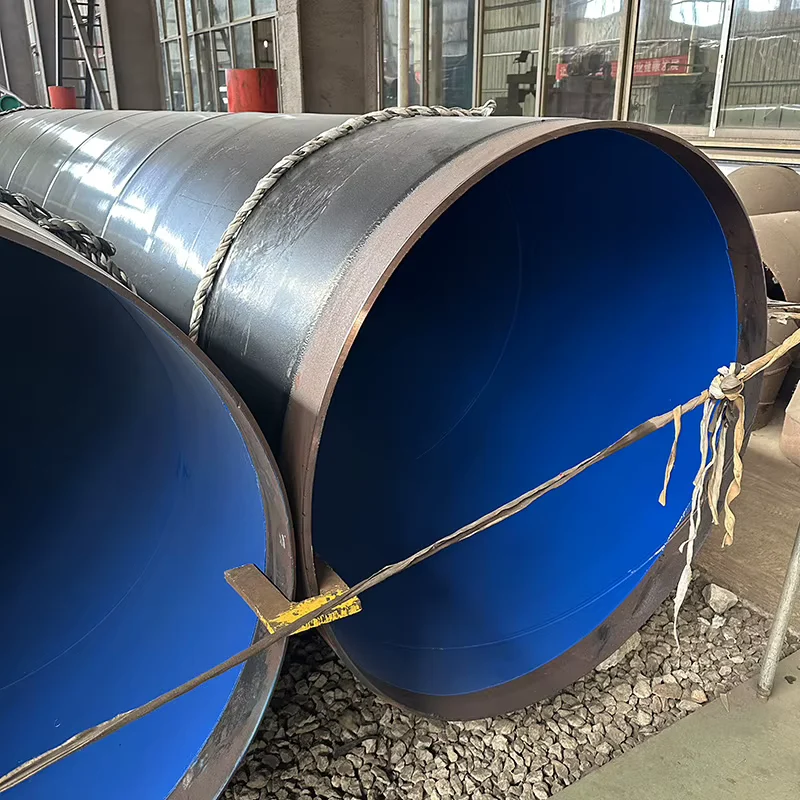
| Surface Treatment | Anti-corrosion coating / Painting / Bare / FBE / 2PE / 3PE / 3PP |
| Tolerance | ±1% (diameter), ovality <1%, deflection <1/2000 |
| Ends | Plain end / Beveled end / PVC covered |
| Application | Fluid conveyance / Piling projects / Heat-supply networks / Petroleum & natural gas pipelines |
| MOQ | 25 Tons |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Municipal Infrastructure | Water intake mains, stormwater drainage trunks, sewage force mains for city utilities |
| Bridge & Port Construction | Driven piles and casings for bridge piers, quay walls, and offshore platform foundations |
| Oil & Gas Transmission | Buried trunk lines for crude oil, natural gas gathering, and refinery process loops |
| Industrial Plant Piping | Cooling water circulation, mine slurry transport, and chemical feed lines |
| District Energy Networks | Pre-insulated carrier pipes for centralized heating and steam distribution |
How Spiral Seam Geometry Reduces Wall Thickness on Pressure Pipelines
The spiral weld carries 75–90% lower stress than a longitudinal seam at identical internal pressure.
When I first inspected a straight-seam pipe order for a West African water project, the mill had quoted DN400 with wall thickness calculated for LSAW — but the client’s pressure rating actually allowed a thinner wall if we switched to SSAW. The spiral seam distributes hoop stress along the helix angle, meaning you can spec a thinner wall for the same design pressure. That 10–25% wall reduction translates directly into lower tonnage, lower freight cost, and easier handling on site. The catch is that not every mill holds the forming precision to keep ovality under 1% at 2200 mm OD — and that is where field-fit failures begin. [NEED_CITE: spiral welded pipe stress distribution versus longitudinal seam]
Matching Large-Diameter Spiral Pipe to Buried and Piling Environments
A DN400–DN2200 SSAW spiral welded steel pipe must survive decades of soil contact, stray current, and hydrostatic loading. For municipal water and gas mains, 3PE or FBE coating provides dielectric isolation that bare or painted pipe cannot. For driven piling, the pipe needs sufficient ductility in Q345B to absorb impact energy without cracking at the spiral weld — and beveled ends with PVC covers keep threads clean until the field weld crew arrives. We produce the full OD and wall range from a single mill, so the piling contractor does not need to split orders across three suppliers.
Engineering Compliance and Certification Pathways
Large-diameter spiral pipe for pressure service must conform to API 5L for oil and gas, or SY/T5037 / GB/T9711 for water and structural piling in China. For EU projects, the equivalent framework is EN 10219 for cold-formed sections, though SSAW for pipeline use typically follows API 5L PSL1/PSL2 with supplementary Charpy testing at specified temperatures. [NEED_CITE: API 5L PSL2 supplementary testing requirements] Dimensional tolerance — ±1% on OD, ovality <1%, deflection <1/2000 — ensures that field weld joint preparation stays within code without costly re-machining. Third-party inspection by SGS or BV before shipment closes the documentation loop for customs and owner-engineer approval.
Steel Grade Selection and Spiral Welding Fundamentals
Q235B and Q345B cover the majority of water, drainage, and piling applications — Q235B for general structural and low-pressure fluid service, Q345B where higher yield strength reduces wall thickness on deeper burial or higher-pressure mains. For oil and gas transmission, API 5L grades from X42 through X80 provide the required strength-toughness balance for sour service and low-temperature operation. The SSAW process forms the pipe continuously from a coiled strip, with the spiral seam advancing at a helix angle that spreads forming stress across a longer weld length — this is why a single strip can produce a 2200 mm OD pipe without the width limitation of plate for LSAW. Metal utilization improves by 6–8% compared to straight-seam forming, and longer single-pipe lengths reduce the number of field girth welds.
Hidden Costs of Specifying the Wrong Tolerance or Coating
A pipe that passes mill inspection but fails third-party holiday detection on its 3PE coating will be rejected at the port — or worse, buried and leaking within two years. Negative tolerance beyond the code-allowed limit reduces the actual pressure rating, forcing the owner-engineer to order hydrostatic re-testing or full replacement. [NEED_CITE: negative tolerance impact on pressure rating in pipeline standards] Missing heat-number traceability on the mill test certificate blocks customs clearance in regulated markets. The cost of re-ordering, re-shipping, and project delay always exceeds the price difference between a qualified mill and a trader blending stock from unknown sources.
Why Project Procurement Teams Source SSAW Pipe from Our Mill
We operate three dedicated production lines covering over 2,800 specifications, so a single order for DN400 water main, DN800 piling casing, and DN1200 gas trunk line ships from one mill with consistent chemistry and coating quality. Our in-house physical and chemical laboratory issues mill test certificates per heat number — no third-party lab markup, no waiting for external test slots. We hold ISO 9001:2015, Lloyd’s CE certification for EN 10210/10219, Singapore FPC, and SGS/BV verified status, which means your customs broker receives complete documentation on the first submission. Custom non-standard lengths, beveled ends, and multi-layer coating (FBE, 2PE, 3PE, 3PP) are produced in-house, so you do not pay a coating subcontractor’s margin. Professional container loading with anti-damage measures prevents the bending and surface scratches that cause field rejection — I draw every loading plan myself.
Documentation & Compliance
- Mill test certificate documenting Q235B / Q345B chemical composition and mechanical properties per GB/T9711 or API 5L, traceable by heat number
- API 5L certification for X42–X80 pipeline grades with PSL1/PSL2 test reports
- CE certificate per EN 10210 / EN 10219 for EU market structural and pipeline applications
- SGS or BV third-party inspection report covering dimensional check, coating thickness, and holiday detection
- Material traceability report linking each pipe to its heat number, strip coil, and welding pass record
- Full customs documentation set: packing list, bill of lading, certificate of origin, and coating specification sheet
Packaging, Loading & Delivery
- Bare or coated SSAW pipes bundled with galvanized steel strips at 1.5 m intervals, with PVC end caps on beveled ends to protect weld prep during ocean transit
- 3PE / FBE coated pipes wrapped with PE sheet and edge protectors to prevent coating gouge from contact with adjacent pipes or container walls
- DN219–DN600 pipes loaded nested in 20ft or 40ft containers to maximize payload; DN800–DN2200 shipped as breakbulk or flat-rack with cradle supports
- Custom cut-to-length service available for 5.8 m, 6.0 m, 11.8 m, or project-specified lengths to reduce field cutting waste
- Heat number, steel grade, OD, WT, and length stenciled on each pipe in weatherproof paint for site identification
- FOB, CIF, and DDP terms available with door-to-door tracking until arrival at project site
Getting Your SSAW Pipe Order Quoted and Verified
Send us the outer diameter, wall thickness, steel grade, coating type, total tonnage, and destination port — we return a detailed quotation with unit price, production lead time, and shipping terms within 12 hours. If your project requires non-standard OD/WT combinations or specific API 5L grade testing, we confirm feasibility and mill test certificate scope before you commit.
Request Your SSAW Spiral Welded Pipe Quotation
Submit your pipe dimensions, steel grade, coating requirement, and order quantity to receive a detailed price and mill test certificate preview.
Shandong Xin Jiyuan Special Steel Tube Co., Ltd
Website: www.sdxjypipe.com
Tel: +86 531 8573 6315
Mobile/WhatsApp/WeChat: +86 188 5315 7756
Email: admin@sdxjypipe.com
Address: No.11889, Jingshi West Road, Lulian Group, Jinan City, Shandong Province, China
Frequently Asked Questions
Q: What is the difference between SSAW, LSAW, and ERW pipe for large-diameter projects?
A: SSAW spiral welded steel pipe is formed continuously from coiled strip with a helical weld seam, allowing production of large diameters up to 2200 mm from narrower strip. LSAW uses plate pressed and welded along a straight longitudinal seam, suitable for very heavy walls but limited by plate width. ERW is resistance-welded for smaller diameters and thinner walls. SSAW offers lower seam stress, longer single lengths, and better metal utilization for water, gas, and piling applications.
Q: How do I select the right API 5L grade for my pipeline design pressure?
A: API 5L grades from X42 to X80 provide increasing minimum yield strength for higher design pressures or deeper burial. X42 and X52 suit low-to-medium pressure water and gas distribution. X60 and X70 are standard for onshore transmission lines. X80 is used for high-pressure long-distance pipelines. The selection depends on design pressure, wall thickness, operating temperature, and whether sour service (H2S) testing is required.
Q: Which anti-corrosion coating is best for buried water or gas pipelines?
A: 3PE (three-layer polyethylene) provides the highest mechanical protection and moisture resistance for buried pipelines in aggressive soils. FBE (fusion-bonded epoxy) offers excellent adhesion and cathodic disbondment resistance, often used as the base layer under 3PE or alone for moderate conditions. 2PE and 3PP are alternatives for specific temperature or chemical exposure. Bare or painted pipe is suitable only for temporary or above-ground service.
Q: How is dimensional tolerance controlled on large-diameter SSAW pipe above 1000 mm OD?
A: Our SSAW lines maintain ±1% on outer diameter, ovality below 1%, and deflection less than 1/2000 through continuous forming control and in-line ultrasonic measurement. This ensures field weld joint preparation meets code without re-machining, and that nested container loading does not cause interference or coating damage.
Q: What is the policy on negative wall thickness tolerance for SSAW pipe orders?
A: We produce to the positive side of the tolerance band specified in API 5L, GB/T9711, or SY/T5037. Every pipe is measured and documented on the mill test certificate with actual wall thickness at multiple points. We do not supply pipe with negative tolerance beyond the code-allowed limit, ensuring the actual pressure rating matches the design calculation.