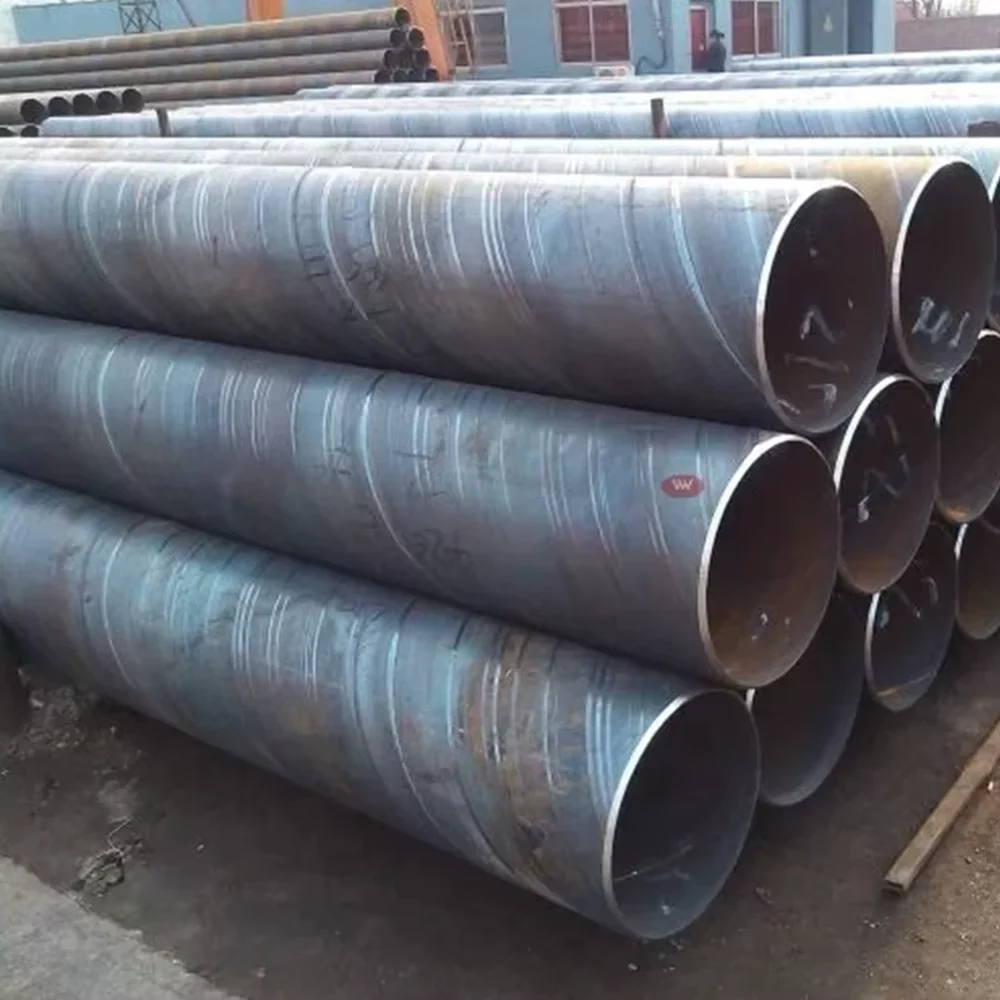
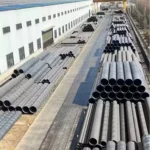
Description
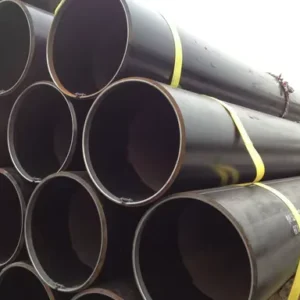
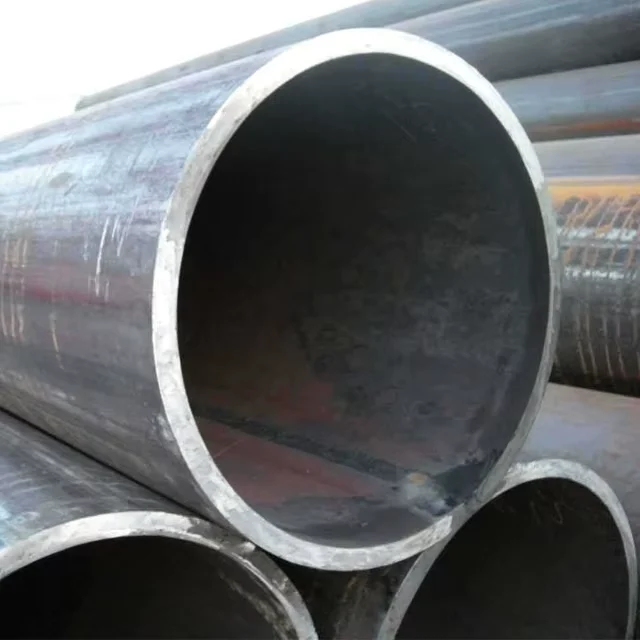
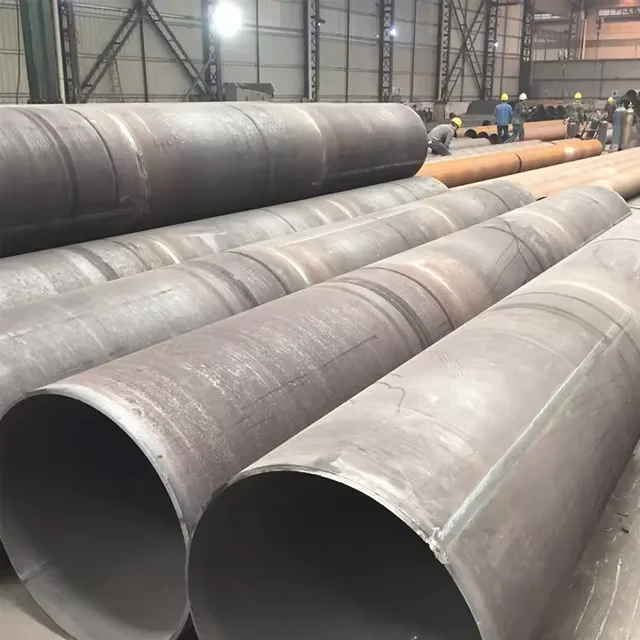
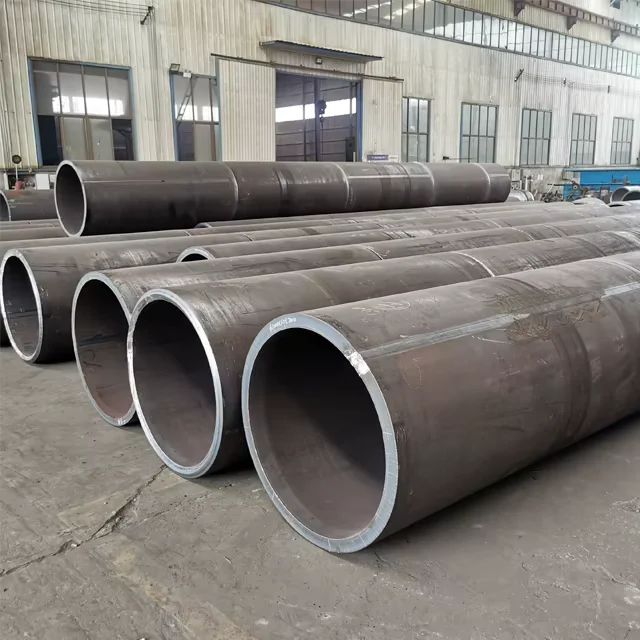
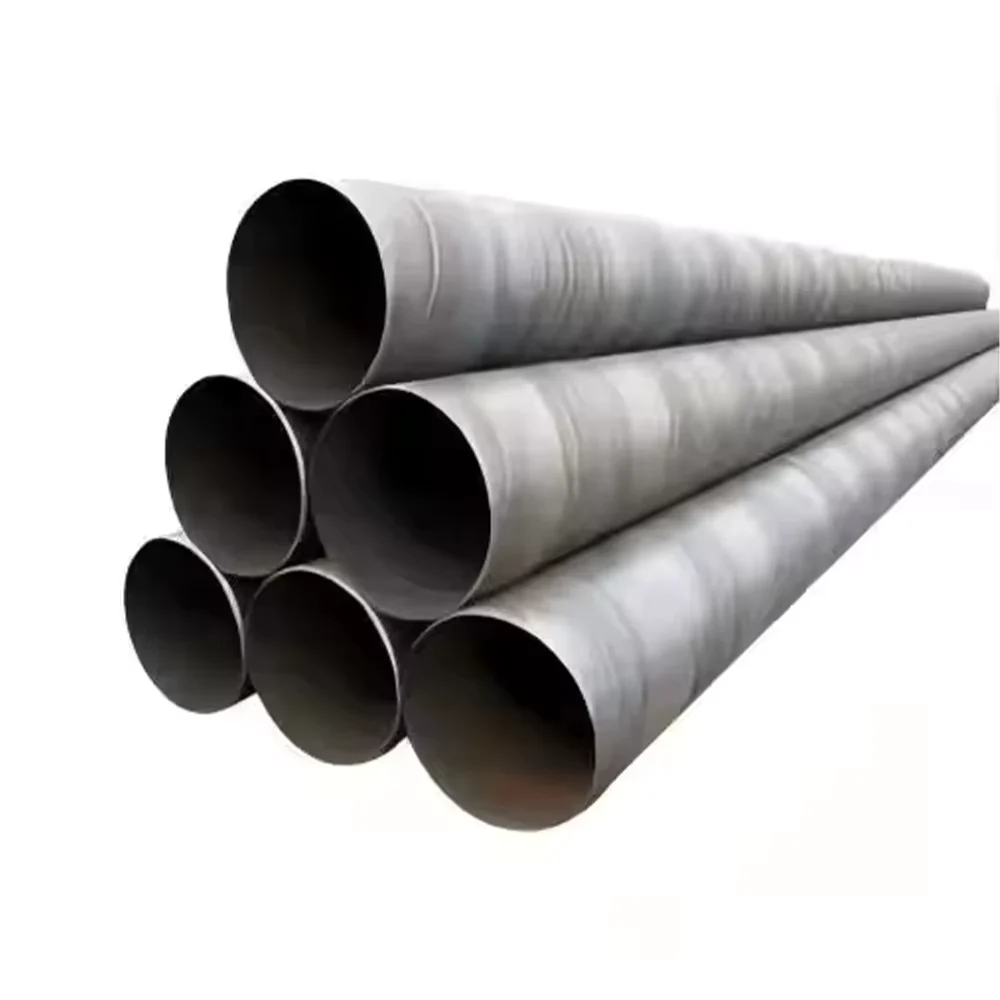
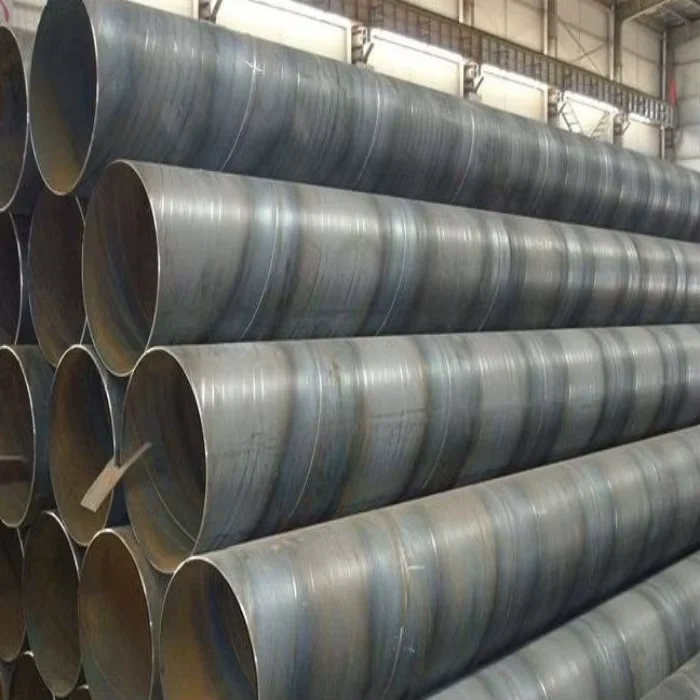
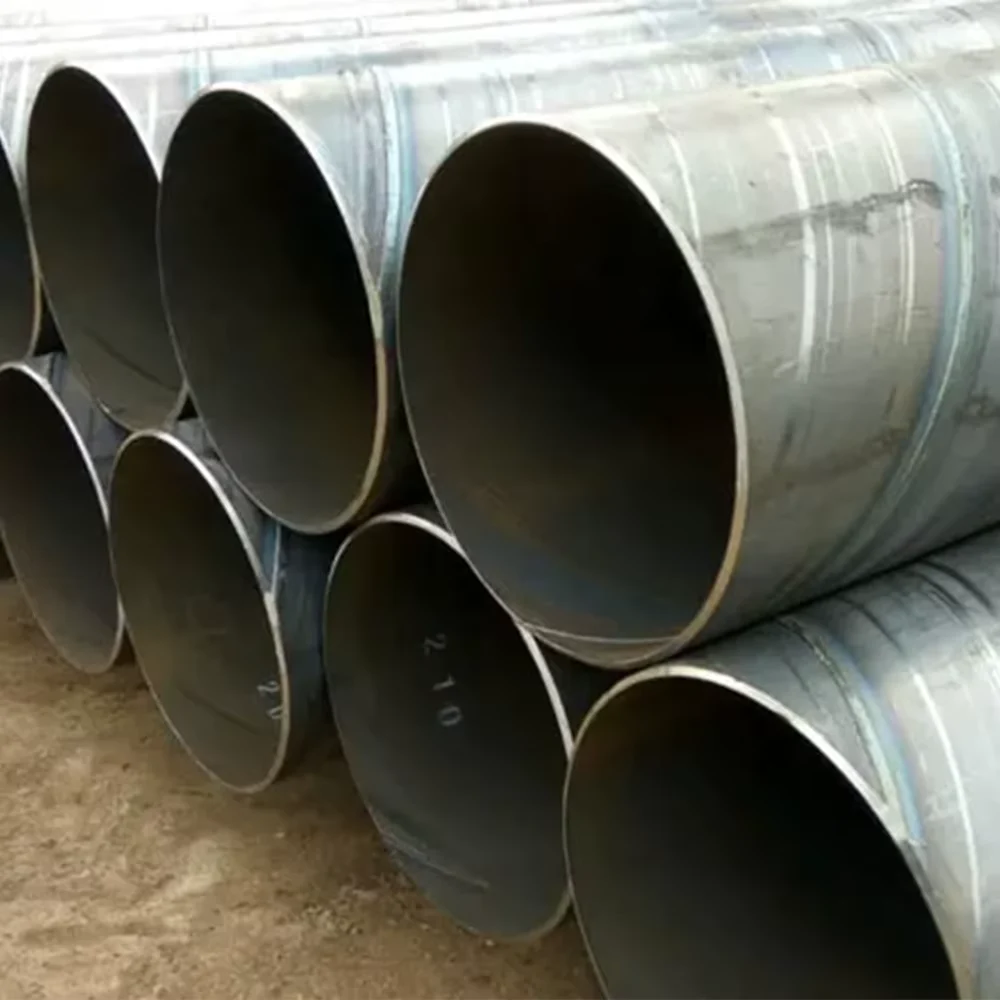
Factory-Direct SSAW Pipe Mill — We produce hot dipped galvanized spiral welded steel pipe in-house from coil to finished coating, cutting out trading margins on API 5L X42–X70 orders.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | API 5L X42-X70 Spiral Welded Steel Pipe |
| Product Type | Spiral Welded Steel Pipe (SSAW) |
| Steel Grade | API 5L X42, X52, X60, X70 / L245, L290, L360, L390, L415, L485 / P235GH, P265GH / Q195, Q235, Q345 / ASTM A53, A106, A500 / S235JR, S355JR / SS400, St37, St52 |
| Standard | API 5L, EN 10217, ASTM A53, ASTM A106, ASTM A500, GB/T 3091, GB/T 13912, BS 1387 |
| Section Shape | Round |
| Size Range | Outer Diameter 219mm–3000mm |
| Wall Thickness | 6mm–25mm |
| Length | 6m–12m (or customized) |
| Technique | Hot Dipped Galvanized, Spiral Welded (SSAW) |
| Surface Treatment | Hot Dipped Galvanized / Black Painting |
| Tolerance | ±1% |
| Ends | Plain / Beveled (per API 5L) |
| Application | Fluid transport (oil, gas, water) / Boiler pipe / Structural pipe / Construction pipe / Chemical fertilizer pipe / Pipeline engineering |
| MOQ | 5 Tons |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Oil & Gas EPC | Onshore and offshore transmission pipelines, gathering lines, and process piping |
| Municipal Infrastructure | City water supply mains, sewage discharge networks, stormwater drainage |
| Piling & Foundation | Bridge piers, wharf structures, and retaining wall piles |
| Industrial Plant | Cooling water circuits, chemical fertilizer feed lines, boiler feed systems |
| Construction | Structural columns, truss members, and scaffold support posts |
Why Zinc Coating Thickness Determines Pipeline Acceptance on Site
A galvanized pipe that fails the micrometer test at destination gets rejected — regardless of how competitive the price was.
I once shipped a batch of hot dipped galvanized spiral welded pipe to the Middle East. The site supervisor pulled out a coating thickness gauge, checked a random pipe, and read 45 microns. The contract specified 80 microns minimum. The entire lot was flagged for re-galvanizing. Since that day, I have treated coating consistency as a non-negotiable checkpoint before any shipment leaves the yard. Inconsistent zinc coverage leads to premature corrosion, weld-line peeling, and ultimately project rejection — costs that far exceed the price difference between a reliable mill and a questionable one. [NEED_CITE: hot dip galvanized coating thickness requirements per ISO 1461 and ASTM A123]
Matching Large-Diameter SSAW Pipe to High-Pressure Pipeline Environments
Hot dipped galvanized spiral welded steel pipe API 5L X42–X70 covers outer diameters from 219mm up to 3000mm with wall thicknesses reaching 25mm, making it suitable for both high-pressure fluid transmission and heavy structural piling. The spiral submerged arc welding process allows continuous production of large diameters that straight-seam mills cannot reach economically, while the hot dip galvanizing bath provides a metallurgical zinc-iron bond that resists mechanical damage during handling and burial. Our in-house physical and chemical laboratory tests every heat for coating adhesion, zinc layer uniformity, and weld integrity before release.
Engineering Compliance Across API, EN, and GB Standards
Pipeline projects often require the pipe to satisfy multiple code frameworks simultaneously — API 5L for North American oil and gas operators, EN 10217 for European water and process lines, and GB/T 9711 for domestic Chinese energy infrastructure. Grade equivalence becomes critical here: API 5L X42 maps to L245, X52 to L360, X60 to L415, and X70 to L485 under the ISO 3183 designation system. Selecting the correct grade ensures that design calculations for hoop stress, allowable working pressure, and low-temperature toughness remain valid under the governing code. [NEED_CITE: steel grade equivalence mapping between API 5L and EN 10217] End preparation — plain or beveled per API 5L — must match the field welding procedure specification to avoid fit-up gaps that compromise root pass quality.
Decoding SSAW Process and Hot Dip Galvanizing for Pipeline Use
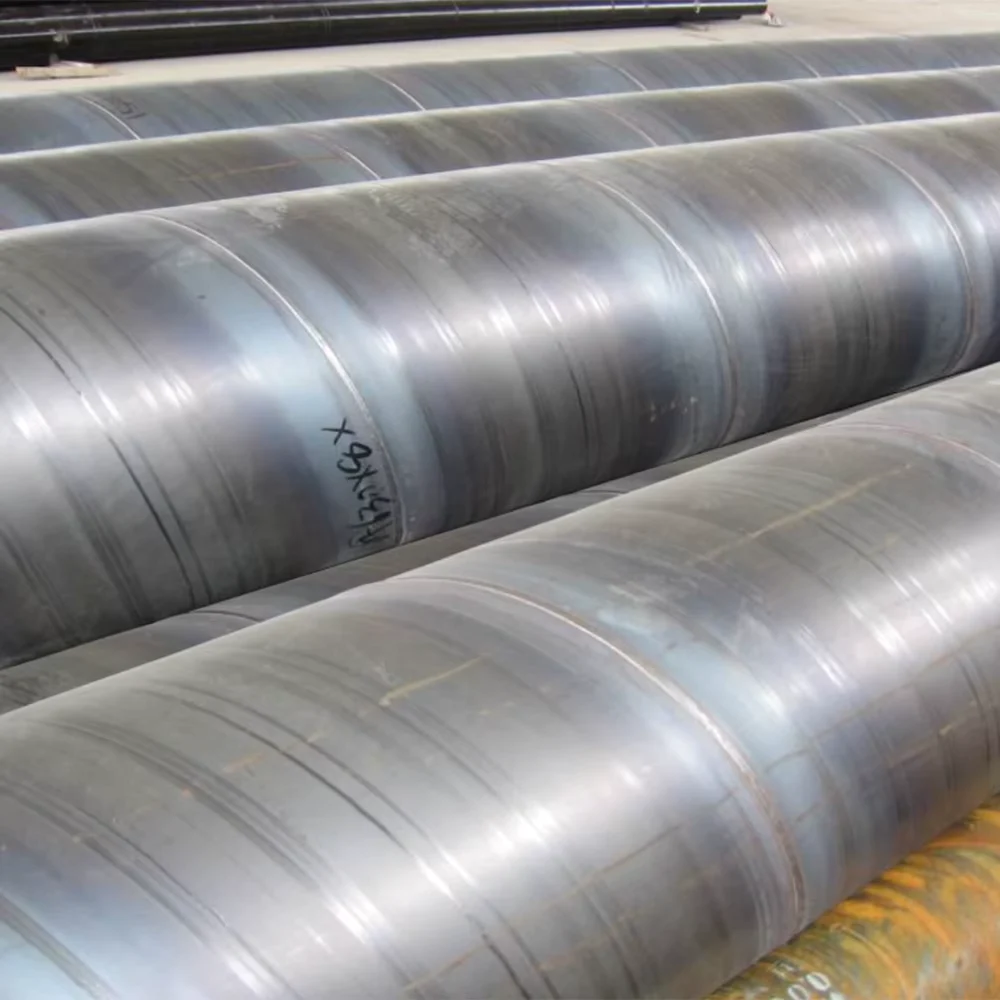
Spiral submerged arc welding forms the pipe from a coiled steel strip at a helical angle, distributing weld stress more evenly than a single straight seam and enabling diameters up to 3000mm from standard-width plate. This geometry makes SSAW the preferred choice for large-diameter water transmission and piling where straight-seam or seamless alternatives become cost-prohibitive. After forming and weld inspection, the pipe enters the hot dip galvanizing line: it passes through a flux bath, then a molten zinc bath at approximately 450°C, where a series of zinc-iron alloy layers form on the steel surface. The resulting coating provides barrier protection, cathodic protection, and mechanical resistance in a single system — far more durable than electro-galvanized or paint-only alternatives for buried or submerged service. Wall thickness tolerance of ±1% ensures that theoretical weight calculations remain accurate for structural design, while the ±1% OD tolerance keeps field fit-up within acceptable limits for girth welding.
Hidden Costs of Procuring the Wrong Grade or Unverified Coating
Ordering a lower steel grade than the design specifies — say substituting X42 where X60 is called for — reduces the allowable working pressure and may trigger rejection during hydrostatic testing at the commissioning stage. Similarly, a mill test certificate that lists chemical composition but omits coating thickness data leaves the buyer unable to prove compliance with ISO 1461 or ASTM A123 at site inspection. Customs authorities in the EU and Middle East increasingly require CE marking per EN 10210 or EN 10219 together with a Declaration of Performance; missing documentation means the container sits at port accumulating demurrage while the buyer scrambles for paperwork. [NEED_CITE: EN 10219 cold-formed and hot-formed hollow section compliance requirements]
Sourcing Directly from a Mill with In-House Testing and Full Certification
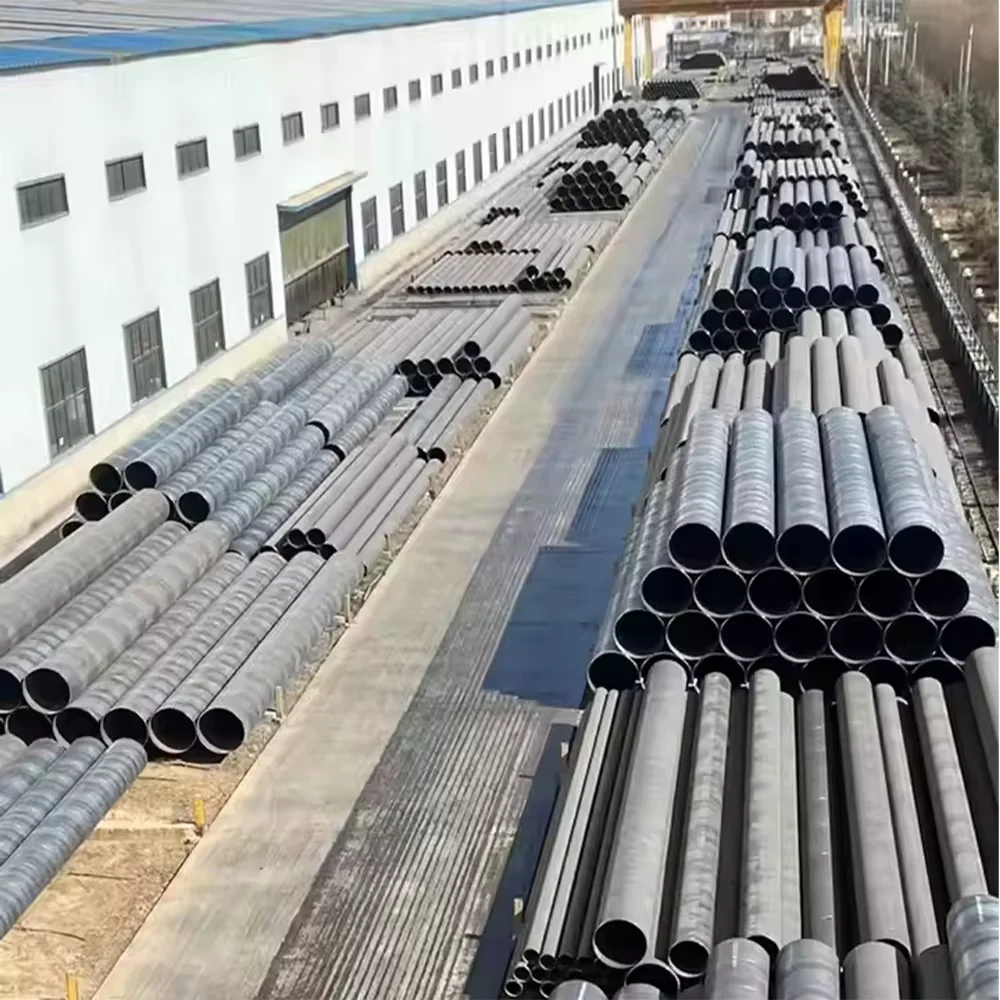
We operate three SSAW production lines covering over 2,800 specification combinations, so your 219mm to 3000mm OD requirement falls within our standard range rather than requiring a special mill run. Every heat is tested in our own physical and chemical laboratory for tensile strength, flattening, bend, and hydrostatic pressure before the pipe reaches the galvanizing kettle. Full international certification — ISO 9001:2015, Lloyd’s CE per EN 10210/10219, Singapore FPC, and SGS/BV third-party verification — means your project engineer receives a complete documentation package without chasing separate suppliers for test reports and certificates. We also hold 41 invention patents and have supplied designated state-owned enterprises and listed companies across more than 50 countries, giving your procurement team a verified reference base.
Documentation & Compliance
- Mill test certificate documenting API 5L X42–X70 chemical composition, yield strength, and tensile properties per heat number, conforming to EN 10204 3.1 or 3.2 as required
- CE certificate per EN 10210 and EN 10219 for hot dipped galvanized spiral welded steel pipe API 5L destined for EU member states
- ISO 9001:2015 quality management certificate covering the full production chain from coil slitting through galvanizing and final inspection
- SGS or BV third-party inspection report verifying coating thickness, dimensional tolerance, and weld quality before container sealing
- Material traceability report linking each pipe to its heat number, coil identity, and galvanizing bath batch for full chain-of-custody documentation
- Export customs documents including packing list, ocean bill of lading, and certificate of origin formatted for the destination country’s import requirements
Packaging, Loading & Delivery
- Hot dipped galvanized spiral welded steel pipe API 5L bundled with high-tensile steel strips and separated by rubberized edge protectors to prevent zinc coating abrasion during ocean transit
- Pipes loaded in nested configuration for OD 219–600mm to maximize container payload; large-diameter pipes above 800mm shipped as breakbulk or on flat racks with timber cradles
- Pipe ends fitted with plastic caps to protect beveled or plain ends and prevent moisture ingress into the bore during container stuffing and sea freight
- Heat number and steel grade stenciled on each pipe in weather-resistant paint, with bundle tags matching the mill test certificate for rapid site identification
- Custom cutting to project-specified lengths within the 6m–12m range, with cut ends re-touched by cold galvanizing spray to maintain corrosion protection continuity
- Shipping terms available as FOB, CIF, or DDP, with professional container loading supervision and real-time tracking until arrival at the destination port or project site
Submit Specifications to Receive a Detailed Quote and Mill Test Certificate
Send your required outer diameter, wall thickness, steel grade, quantity, and destination port, and we will return a detailed quotation including unit price, typical production lead time, and shipping terms within 12 hours. We can also arrange SGS or BV third-party inspection and provide sample pipes with full mill test certificates for your engineer’s approval before contract signing.
Get Your API 5L SSAW Pipe Quote with Full Certification Package
Share your pipe specifications, steel grade, and destination to receive a quotation and mill test certificate. Contact us at +86 188 5315 7756 (WhatsApp/WeChat) or email admin@sdxjypipe.com.
Frequently Asked Questions
Q: What is the grade equivalence between API 5L and EN 10217 for spiral welded pipe?
A: API 5L X42 corresponds to L245, X52 to L360, X60 to L415, and X70 to L485 under the ISO 3183 designation system used by EN 10217. We supply hot dipped galvanized spiral welded steel pipe API 5L in all these grades and can provide a cross-reference chart with your inquiry.
Q: How does hot dip galvanizing compare to electro-galvanizing for pipeline service?
A: Hot dip galvanizing produces a metallurgical zinc-iron alloy coating significantly thicker than electro-galvanized layers, providing both barrier and cathodic protection suitable for buried and submerged pipeline environments. Electro-galvanized coatings are thinner and better suited for indoor or decorative applications where appearance matters more than long-term corrosion resistance.
Q: Can you arrange third-party inspection before shipment?
A: Yes. We coordinate SGS, BV, or Lloyd’s inspection at our facility before container loading. The inspector verifies coating thickness, dimensional tolerance, weld quality, and end preparation, and issues a report that accompanies the mill test certificate in the shipping documentation package.
Q: How do you handle container loading for large-diameter SSAW pipe?
A: Pipes with outer diameter up to approximately 600mm are nested inside standard containers to maximize weight utilization. Larger diameters above 800mm are loaded on flat racks or shipped as breakbulk with timber cradles and steel strapping to prevent rolling and surface damage during transit.
Q: What is the minimum order quantity for hot dipped galvanized SSAW pipe?
A: The minimum order quantity is 5 tons. Standard sizes may ship from stock, while custom outer diameter and wall thickness combinations enter the production schedule with typical lead times confirmed at the quotation stage.
Request Your Hot Dipped Galvanized SSAW Pipe Quotation Today
Provide your OD, WT, grade, and quantity to receive a detailed offer with mill test certificates and third-party inspection options. Reach us at +86 188 5315 7756 or admin@sdxjypipe.com.